If you’re in the bearing manufacturing game, you’ve probably heard folks throw around terms like “forming speed” when talking about bearing ring formers—and if you’re a shop owner trying to hit your production targets without ditching quality, that question’s probably been bouncing around your head more than once. Let’s break this down like we’re grabbing a coffee after a long shift, no stuffy whitepaper jargon, just straight talk from someone who’s spent years selling and working with these machines. Bearing Ring Former
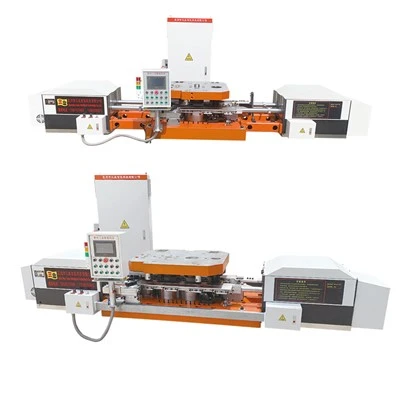
First off, let’s get one thing straight: forming speed isn’t just a random number we pull out of thin air. It’s the rate at which a bearing ring former shapes hot metal (usually steel or alloy, depending on the bearing’s use case) into that perfect round, hollow ring we all know. For context, bearing rings are the core of any ball or roller bearing—mess up their shape, and your whole bearing’s gonna fail faster than a cheap fan in a dusty factory. That’s why this speed matters so much.
When a former is turning, that speed is measured in strokes per minute (SPM) for mechanical formers, or sometimes meters per second (m/s) for the ram’s movement on hydraulic models. But here’s the kicker: there’s no one-size-fits-all number. Way too many new buyers we chat with expect a “best” speed they can plug in, but it’s way more dependent on what they’re making. Let’s run through the basics first, then get into the stuff that actually affects it.
First, the material. If you’re working with mild carbon steel, you can crank that speed way higher than if you’re using a high-strength alloy like chrome steel (52100) or stainless steel. Why? Alloys are harder, less malleable when hot, and if you push them too fast, you’ll get defects—like cracks, uneven wall thickness, or even wrinkles in the ring. Last year, we had a customer who tried to run their chrome steel rings at 80 SPM on a machine we sold them; they kept getting 12% defect rates until we knocked it down to 55 SPM. Turned out their material needed a slower, more controlled push to shape right.
Then there’s the ring size and thickness. A small, thin ring for a miniature bearing (say, 10mm outer diameter) can fly through the former at 100+ SPM. But a big, thick ring for a heavy-duty industrial bearing—like a 1-meter outer diameter ring for a mining conveyor—needs a way slower speed, often 20 SPM or less. Think of it like shaping clay on a potter’s wheel: a tiny, thin bowl spins fast, but a huge, thick pot needs slower turns to not collapse. Same logic here.
The type of former you’re using also plays a role. There’s mechanical formers, hydraulic formers, and even servo-driven ones these days. Mechanical ones are workhorses—they’re fast, consistent, and good for high-volume, standard rings. A servo-driven former, on the other hand, lets you adjust speed on the fly, which is perfect if you’re making mixed batches of ring sizes. We’ve seen mechanical formers hit 120 SPM for small, mild steel rings, while a hydraulic model for thick, large rings maxes out at 30 SPM. That gap isn’t just a random stat—it’s built into how each machine works.
Wait, but what about the forming process itself? Most formers do a few steps: first, they heat the metal blank to around 1200°C (for steel, anyway), then punch it into a rough shape, then size it into the finished ring. The forming speed can shift between steps, too. The roughing step might be faster because you just need to get the general shape, but the finishing step needs slower, more precise movement to make sure the ring’s roundness and tolerance are within that +/- 0.02mm zone bearings require. Mess up the finishing step’s speed, and you’ll have rings that don’t fit the balls or rollers right—leading to noise, vibration, or early failure.
Now, let’s talk about the tradeoff everyone’s scared of: speed vs. quality vs. productivity. A lot of shops want to run as fast as possible to make more rings, but that’s a balancing act. Run too fast, and you’ll have defects, which mean wasted material, rework, and downtime. Run too slow, and you’re not hitting your production targets, which eats into profits. We had a customer a couple years back who tried to max out their servo former at 90 SPM, got 8% defects, so they slowed to 75 SPM, defect rate dropped to 1.5%, and total production output actually went up because they didn’t have to rework half the parts. That’s a key point people miss: sometimes, a slightly slower speed is better for your bottom line in the long run.
Another factor we don’t talk about enough: machine maintenance. If your former’s got worn dies, loose parts, or a hydraulic system that’s slipping, you can’t run it at full speed. We had a new customer bring their old former to us last quarter—they were running it at 60 SPM, but their dies were 3 years old and had nicks. We sharpened the dies, adjusted the alignment, and they were able to run it at 72 SPM without any extra defects. So the forming speed isn’t just about the machine or the material—it’s about how well you’re maintaining the kit.
Now, what’s the general range you can expect? For most standard bearing rings (outer diameter 50mm to 500mm, mild or chrome steel), the sweet spot is between 40 SPM and 80 SPM for mechanical formers, or 0.5 m/s to 1.5 m/s for ram speed. For smaller, high-volume rings, it can go up to 120 SPM, and for heavy-duty, large rings, it’s usually 15 SPM to 30 SPM. But like I said earlier, that’s just a baseline—you have to adjust from there.
Wait, let’s address a common myth: “faster always means better.” Nope, not when it comes to forming. Speed that’s too high creates more heat in the metal than intended, which can mess up the material’s grain structure—something that’s super important for bearing durability. A bearing’s gotta handle millions of rotations, so if the grain’s messed up from too-fast forming, it’ll crack under pressure. We’ve tested this with customer samples: rings formed at 90 SPM had a 3x higher fatigue failure rate than those at 65 SPM, even if they looked identical on the surface.
So, what should you do if you’re setting up or tweaking your bearing ring former’s speed? First, know your material and part specs. If you’re working with a new alloy, test a few batches at different speeds to find the sweet spot. Second, factor in your machine type—servo formers give you more flexibility, so use that. Third, keep up with maintenance, because even a good machine can underperform if it’s not taken care of. And finally, don’t fixate on the highest number—look at total production cost, including defects and rework.
If you’re still scratching your head, that’s where we come in. We work with shops of all sizes, from small job shops making custom bearing rings to big factories doing high-volume production. We don’t just sell you a machine and leave you to figure out the speed on your own—we help you test your materials, adjust your process, and get that sweet spot that hits both quality and output. A lot of customers come to us complaining about defect rates or missed targets, and more often than not, it’s not the machine—it’s how they’re using its forming speed.
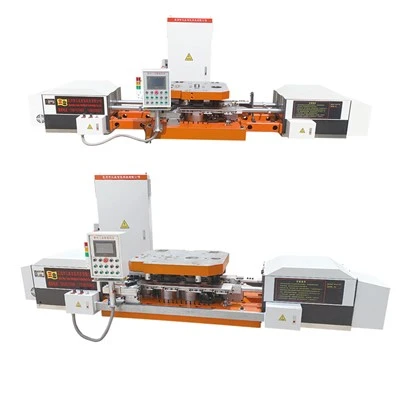
At the end of the day, forming speed is one of the most critical parameters for bearing ring production, but it’s not a one-size-fits-all number. It’s a mix of material, part size, machine type, maintenance, and your own production goals. If you’re looking to upgrade your bearing ring former, tweak your current setup, or just want to chat through what speed makes sense for your specific parts, reach out to our team. We’re happy to break it down, no sales pitch fluff, just honest advice from folks who know this industry inside and out.
Busher Former Machine References
- Kalpakjian, S., & Schmid, S. R. (2020). Manufacturing Processes for Engineering Materials. Pearson Education.
- Bhansali, S. (2018. Metal Forming Science and Practice. CRC Press.
- International Organization for Standardization. (2021). ISO 1101:2021, Geometrical Product Specifications (GPS) — Geometrical tolerances — Tolerances of form, orientation, location and run-out.
Quanzhou Sanye Intelligent Technology Co., Ltd.
As one of the most professional bearing ring former manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized bearing ring former made in China here from our factory. Welcome to contact us for quotation.
Address: Anhai Town, Jinjiang City, Fujian Province, China
E-mail: jack_tmm@163.com
WebSite: https://www.qzsymanipulator.com/
